Machine plans that ignore the mould
Jobs are planned from the mould's running cavities and cycle time, so expected output per shift is known before the job starts.
Injection, blow and roto molding
Built for plastic molding plants, from resin and masterbatch receipt through drying, blending, mould setup, molding, trimming and testing to packing, with machine planning by mould cavity and cycle time, mould shot counts and regrind control.
Plastic molding ERP is business software built around how a molding shop runs. Formezy plans machines by mould cavities and cycle time, records the resin, masterbatch and regrind used in each batch, counts shots and good parts per shift, tracks every mould's shot count and maintenance, and holds parts that fail inspection, so output, scrap and cost per part stay current.
Jobs are planned from the mould's running cavities and cycle time, so expected output per shift is known before the job starts.
Each mould's shot count builds up from production entries, and preventive maintenance falls due by shots, not by memory.
Runners, flash and rejects are weighed back to regrind stock, and the regrind percentage in each batch is recorded.
Segments
3 segments, each with its own shop-floor process flow.
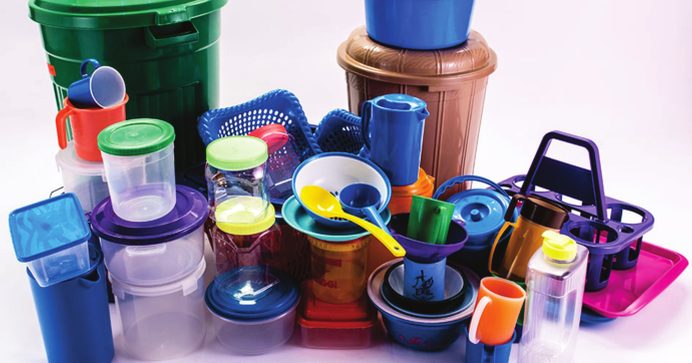
Household items, caps and closures, containers, crates, pharma and engineering parts. Plan by cavity and cycle time, count shots per shift and track every mould.
See the 8-step flowBottles, jerrycans, drums and containers made by extrusion, injection or stretch blow molding. Track blends, cavity output, leak testing and flash returned to regrind.
See the 7-step flow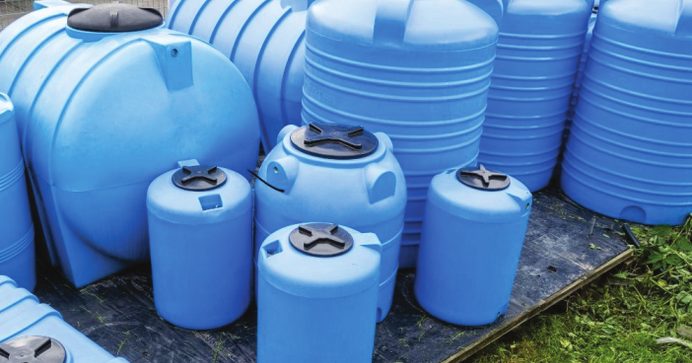
Water tanks, large containers and hollow parts made from roto-grade polyethylene. Charge weights, oven cycles and tank weights recorded per piece.
See the 7-step flowShop-floor process flow
Choose a segment, then a step. Each one shows what happens on the shop floor, what Formezy records, and what changes as a result.
Resin, masterbatch and inserts received and weighed
GRN posts grade, supplier lot no. and weighbridge weight; bags labelled with a lot barcode
Weight Integration moduleResin lot traced from day one
Resin dried where needed and blended with masterbatch and regrind
Blend recipe issued; virgin, regrind and masterbatch weights booked per batch
Production & Purchase moduleRegrind ratio on record
Mould loaded and the machine set for the job
Mould no., running cavities and setup time logged; mould change recorded
Machine Maintenance moduleChangeover time visible
Parts molded shot by shot
Shots, cycle time and stoppages captured per machine; mould shot count updated
IoT & Automation moduleOutput vs. plan, live
First-off and hourly checks for weight, dimensions, flash and short shots
Defects caught at the machine
Quality gate. If it fails: correct the process and send rejects to regrind.
Runners and sprues removed and ground
Scrap weighed, not guessed
Parts counted into bags, cartons or pallets
Finished stock by batch
Cartons loaded against the order
No manual packing lists
Resin, masterbatch and inserts received and weighed
GRN posts grade, supplier lot no. and weighbridge weight; bags labelled with a lot barcode
Weight Integration moduleResin lot traced from day one
HDPE, PP or PET resin and masterbatch received and weighed
GRN posts grade, supplier lot no. and weighbridge weight; bags labelled with a lot barcode
Weight Integration moduleResin lot traced
Virgin resin blended with masterbatch and regrind
Blend recorded per batch
Parisons or preforms blown into containers
Output per machine, live
Flash trimmed and containers weighed
Weight drift spotted early
Containers leak tested; samples checked for weight, wall and fit
Leaking containers never ship
Quality gate. If it fails: reject to regrind.
Containers printed or labelled
Print or label job linked to the batch; consumables booked
Production & Purchase moduleDecoration cost per batch
Containers bagged or palletised and loaded
Order-wise dispatch
HDPE, PP or PET resin and masterbatch received and weighed
GRN posts grade, supplier lot no. and weighbridge weight; bags labelled with a lot barcode
Weight Integration moduleResin lot traced
Roto-grade PE powder or granules and masterbatch received
GRN posts grade, supplier lot no. and weighbridge weight; bags labelled with a lot barcode
Weight Integration moduleMaterial lot traced
Granules ground to powder and coloured with UV-stabilised masterbatch
Powder yield known
Powder weighed into the mould for each product
Material per tank known
Mould heated in the oven while rotating biaxially
Cycle data per piece
Mould cooled and the part removed
Output per arm, live
Weight, wall thickness, finish and leaks checked
Weak tanks never ship
Quality gate. If it fails: repair if allowed, otherwise scrap to regrind.
Fittings and lids added, tanks labelled and loaded
Every tank traceable
Roto-grade PE powder or granules and masterbatch received
GRN posts grade, supplier lot no. and weighbridge weight; bags labelled with a lot barcode
Weight Integration moduleMaterial lot traced
Dashed ring marks a quality gate, where failed material is held before it moves on.
Capabilities
Open an area to see what it covers.
Questions
Talk to a plastic ERP specialist about your own plant and process route.
Formezy supports injection molding, blow molding and roto molding, each with its own process flow. Plants that combine segments run them in one system.
Yes. Each has its own process flow, and plants running more than one molding process, or molding alongside extrusion, work in one system.
Each mould carries its cavities, cycle time and part weight. Planning uses the running cavities and cycle time to work out output per shift, so jobs are matched to suitable machines and delivery dates are realistic.
Yes. Shots booked in production add to each mould's shot count, and preventive maintenance can fall due by shot count or by date, with the history kept against the mould.
Runners, sprues, flash and rejects are weighed back to regrind stock, and blend recipes record the regrind percentage used in each batch, so its use is tracked and costed.
Yes. First-off and periodic checks for weight, dimensions and visual defects are recorded per job, rejects are booked by defect type and suspect batches are held.
Resin, masterbatch, regrind credit, machine time, labour and packing are booked against the job from actual consumption, giving cost per part and per kilogram.
Other industries
See Formezy configured around your own process route, from receipt to dispatch.